Every Core Is Only as Good as the Process Behind It
Sourcing a transformer core from a manufacturer who outsources key processing steps introduces variables you can’t control and tolerances you can’t trust. At Electro-Core, our full processing capability is internal. That means tighter quality control, faster turnaround, and a single point of accountability from material to shipment on every order, regardless of size.
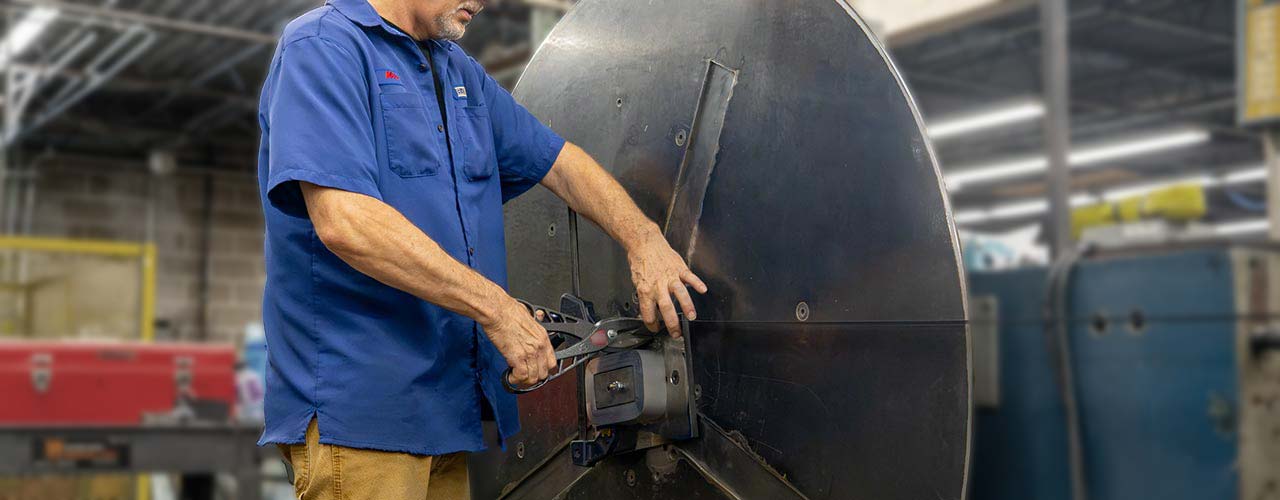
Slitting
In-house slitting lines enable us to process silicon steel to custom widths without relying on outside service centers, a key driver of our lead-time advantage on both standard and custom orders.
Winding
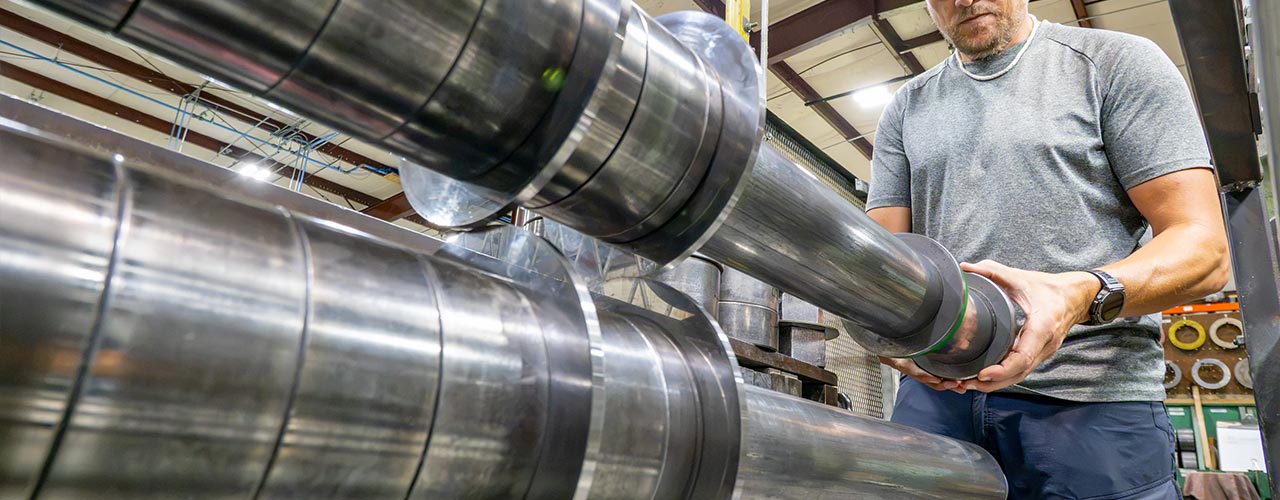
All cores are wound using grain-oriented (GOES) and non-oriented (NOES) electrical steel across the full gauge range, with in-house slitting for custom widths below standard mill minimums.
Annealing
All wound cores are annealed after winding unless otherwise specified. Electro-Core is proud to offer annealing at one of the largest capacities nationwide.
Varnish Impregnation (Bonding)
Cores are vacuum pressure impregnated (VPI) and heat-cured at 450°F. This process must follow annealing and is required on any core that will be cut or gapped.
Edge Bonding
Adds less than 0.002″ to the core surface and is suitable where efficiency is a priority and full varnish impregnation isn’t required. Not applicable for cores that will be cut or gapped.
Cutting
Cutting is standard on all three-phase wound cores. Single- and multi-cut configurations are available, including partial cutting to reduce residual flux. Toroids can also be cut.
Lapping
Precision grinding of cut core mating surfaces, with the degree of lapping specified based on application requirements and cost considerations.
Etching
Applied after cutting or grinding to remove burrs across the lamination stack. Necessity weighed against the efficiency and cost requirements of the application.
Gapping
Gapping is available with Mylar, Nomex, or custom specified material typically for inductor cores or similar applications.
Heat Seasoning
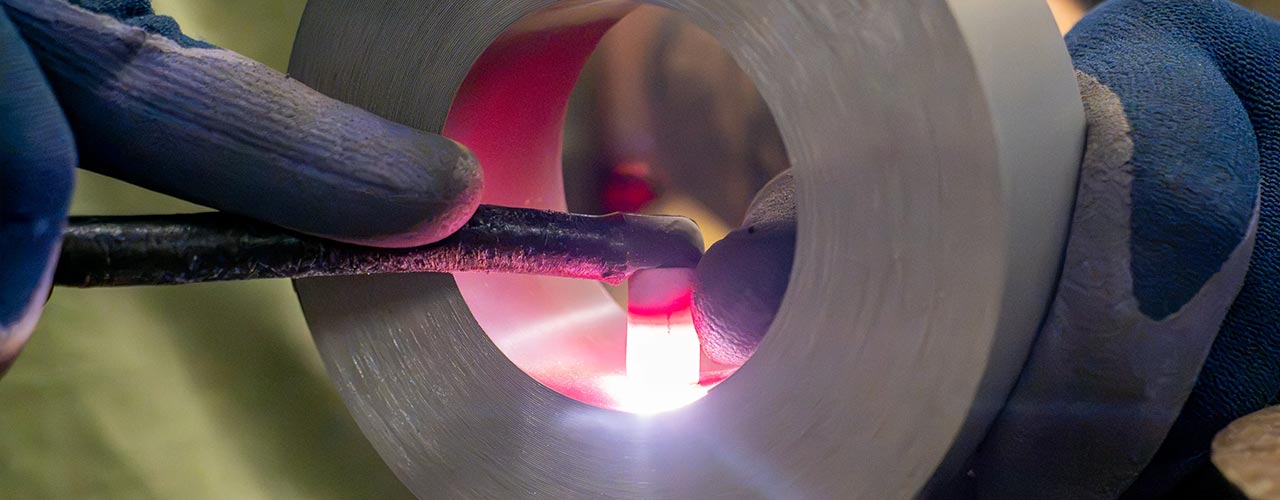
Recommended for any cut core that will operate above 200°F in service. Relieves induced stresses before final finishing to prevent lamination shift and gap enlargement over time.
Epoxy Coating
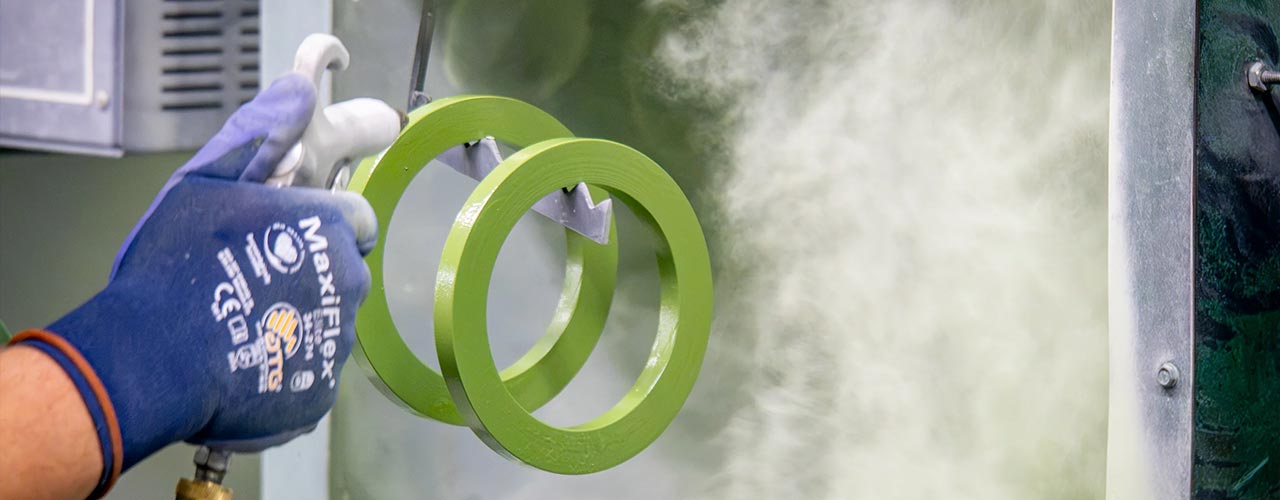
3M #260 electrical resin, UL Recognized (E34-947M) for operation up to 130°C. Standard coating thickness 0.020″ (+0.007″, -0.003″) with a maximum practical thickness of .040”.
Core Caps and Cases
More repeatable external dimensions and greater mechanical protection than epoxy coating alone. Most practical for larger quantity runs due to tooling costs. Can be combined with epoxy coating for maximum protection.
Machining
In-house slotting, special gap machining, drilling, tapping, milling, and grinding. Laminated silicon steel is a difficult material to machine — consult our engineering team early on any project that will require it.
Magnetic Testing
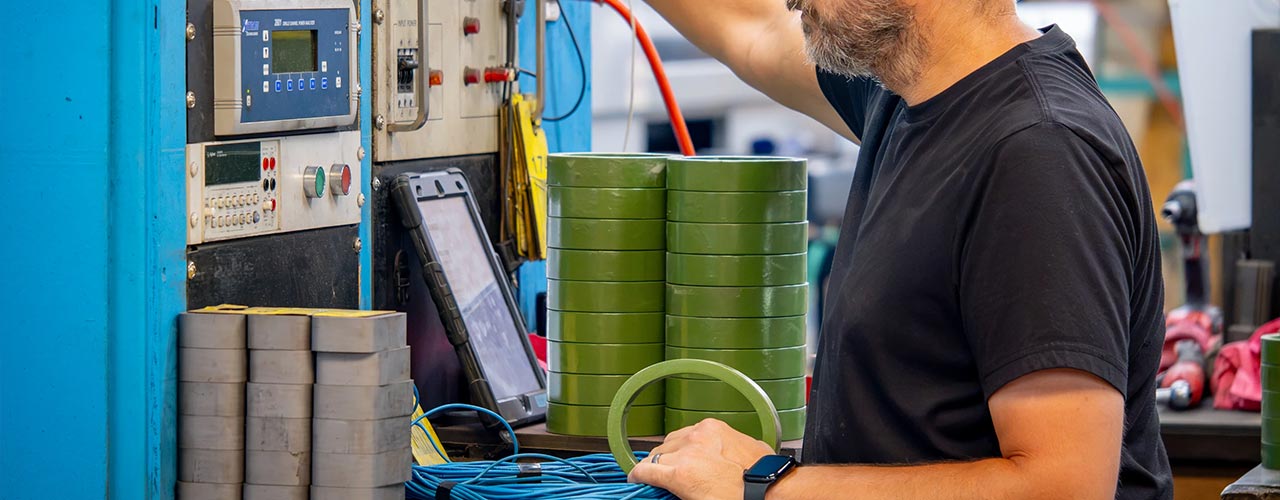
In-house performance verification with empirical performance data available for applications outside standard published magnetic test ranges.
Need a Process Conversation Before You Submit Specs?
Our team has decades of experience working through material selection, process sequencing, and tolerance questions with engineers early in the design cycle — before a problem shows up in production. Reach out before you finalize your specifications.